اتصالات لوله مستقیم Hot Melt Socket Inner Tooth β-Pph 1.0mpa
1. نصب سریع و قابل اعتماد، راحت و صرفه جویی در زمان؛ دیواره های داخلی و خارجی...
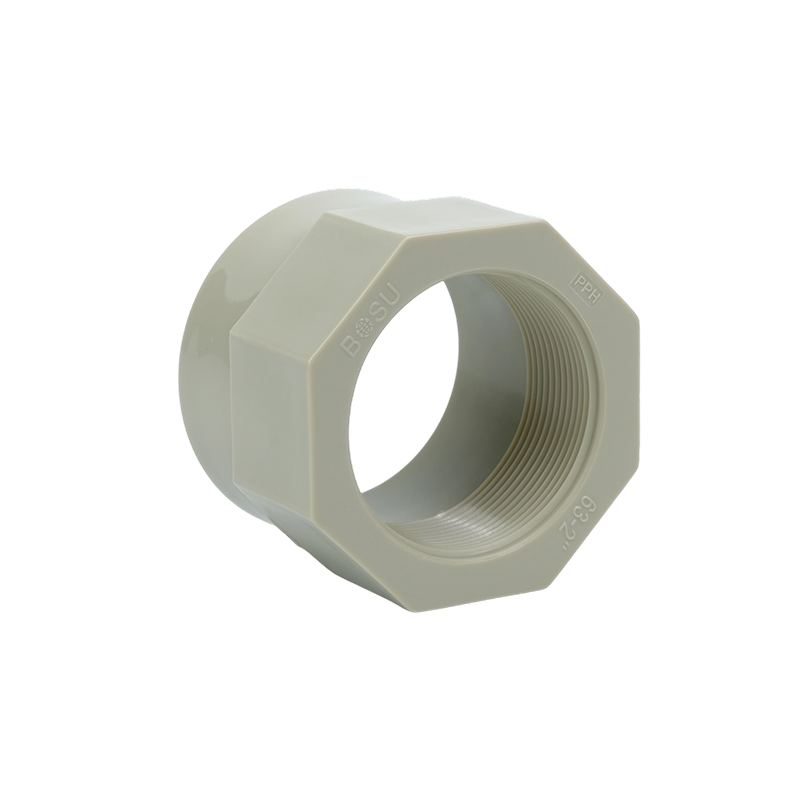
1. نصب سریع و قابل اعتماد، راحت و صرفه جویی در زمان؛ دیواره های داخلی و خارجی...
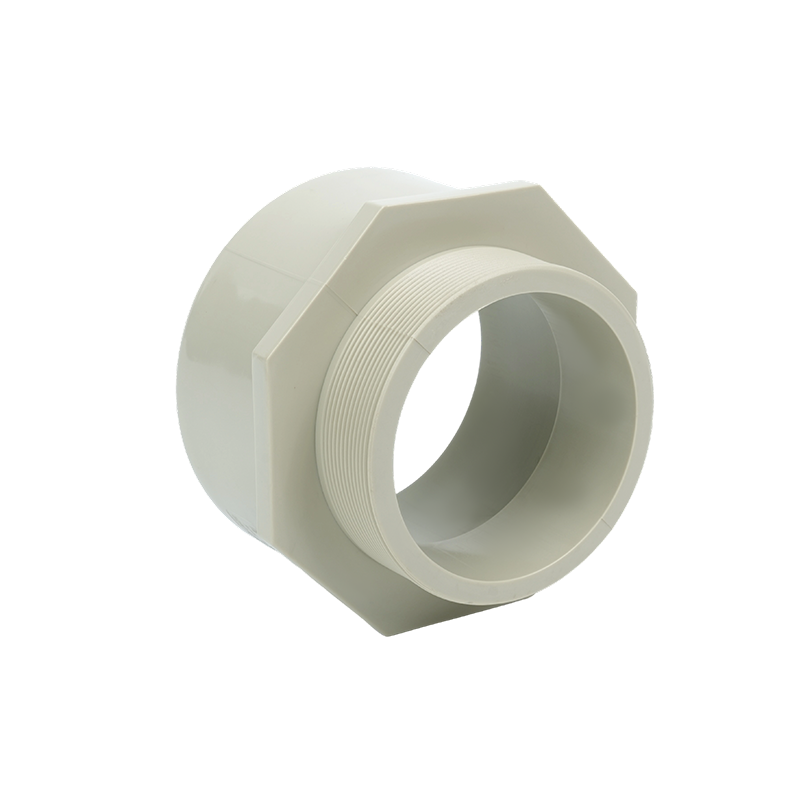
1. عملیات آسان، اتصال قابل اعتماد، مقاومت در برابر فشار بالا، آب بندی خوب، نص...
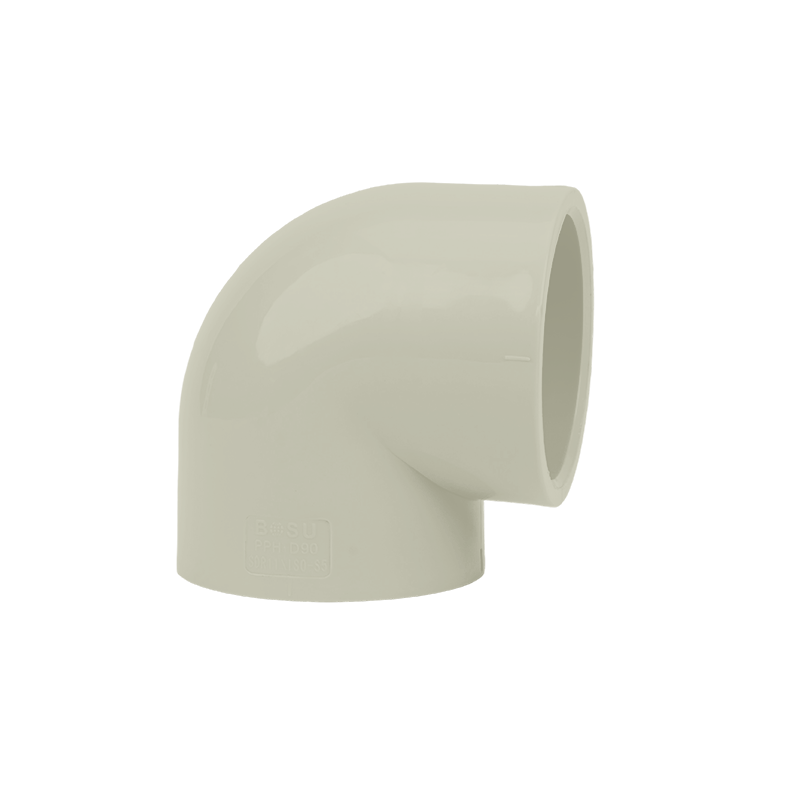
1. برای اتصال در خم لوله، برای تغییر جهت لوله، مناسب برای موارد لوله انشعاب. ...
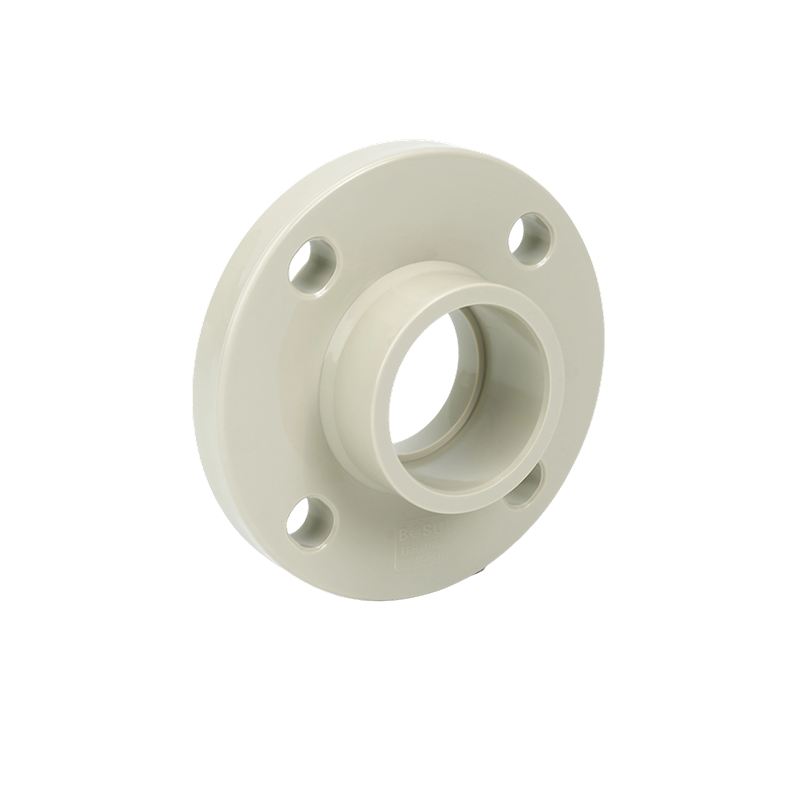
ویژگی های محصول: نصب آسان، این اتصالات به صورت جفت در انتهای لوله استفا...
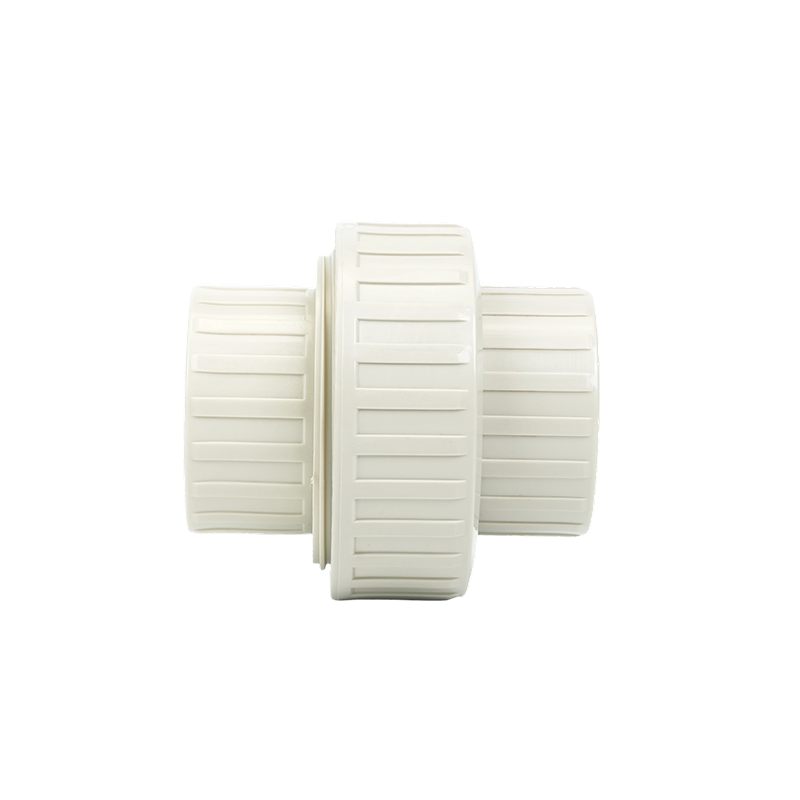
توضیحات: برای اتصال به خطوط لوله با انتهای رزوه ای طراحی شده است. حلقه آب بند...
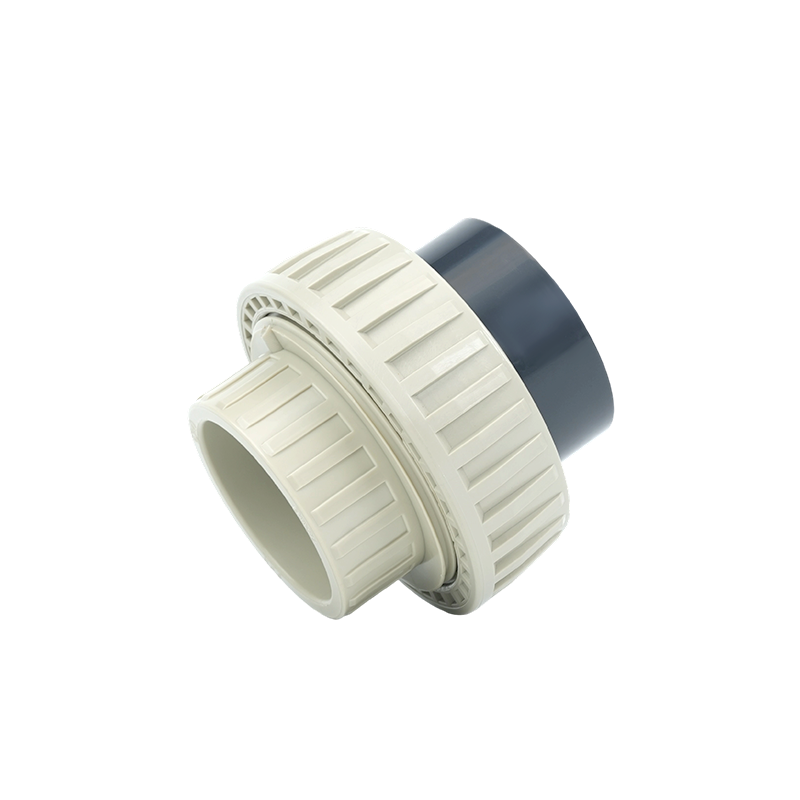
توضیحات: این اتصالات ترموپلاستیک، لولهها را به یک سیستم خط لوله کامل متصل می...
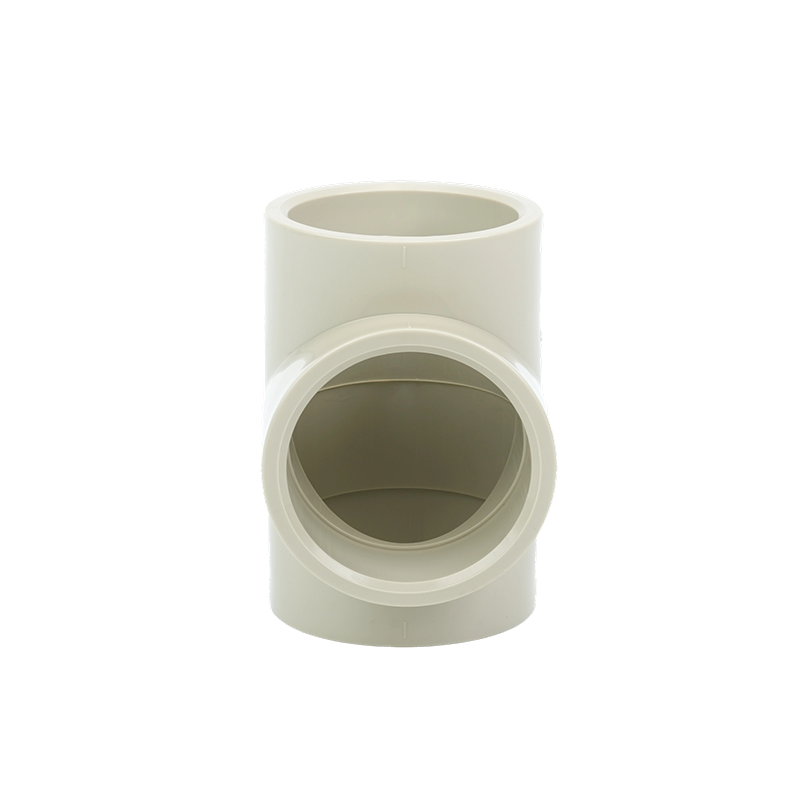
1. متعلق به یکی از اتصالات لوله است که در لوله انشعاب خط لوله اصلی استفاده می...
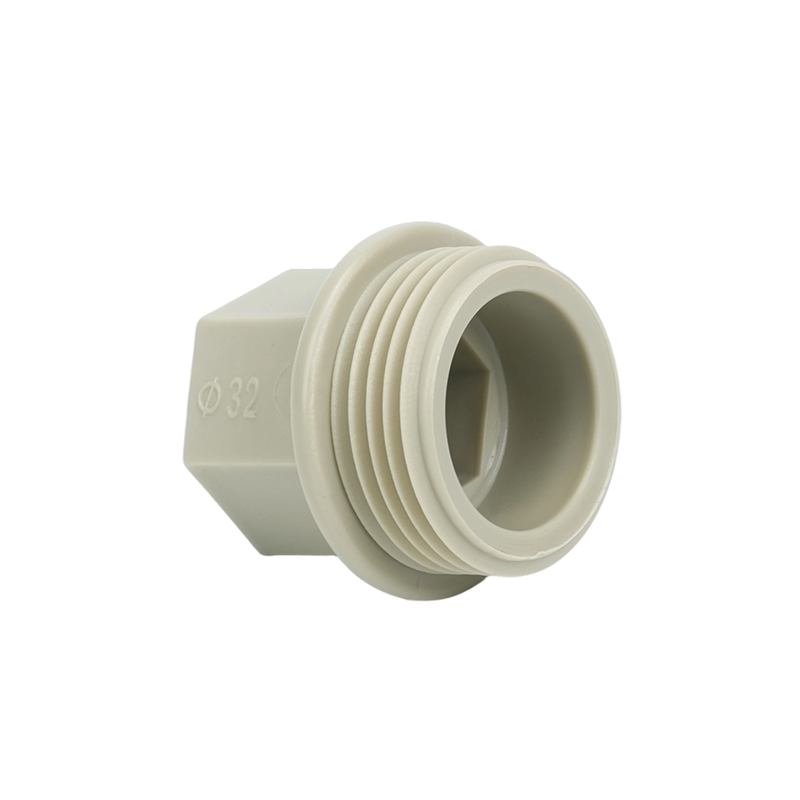
1. بادوام، ضد خوردگی، وزن سبک، عملکرد به عنوان یک خط لوله بسته، نصب و نگهداری...
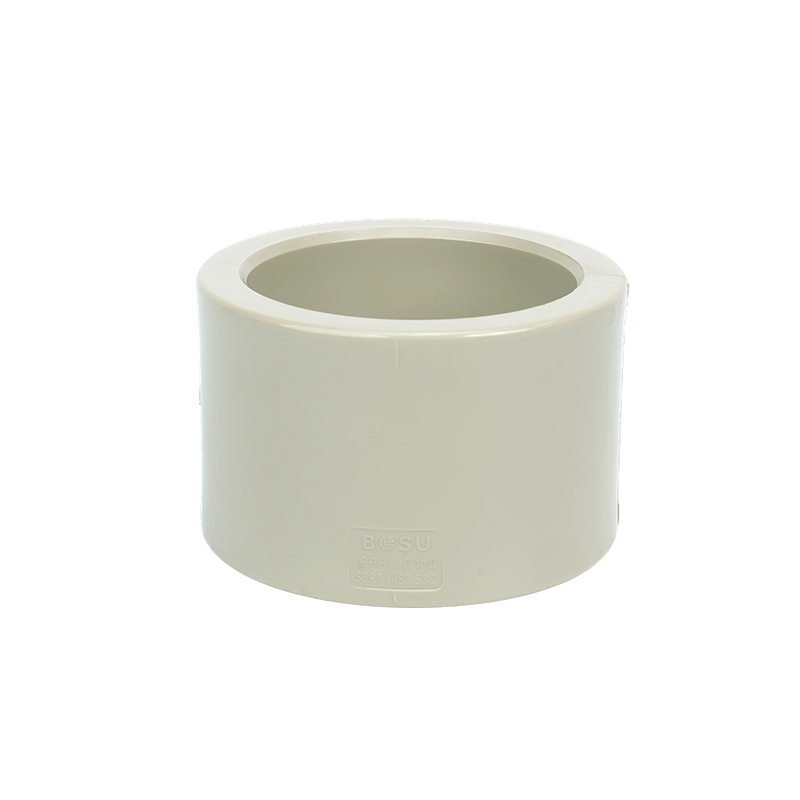
در سیستم های لوله کشی که نیاز به اتصالات انتهایی ساده دارند استفاده می شود. ...
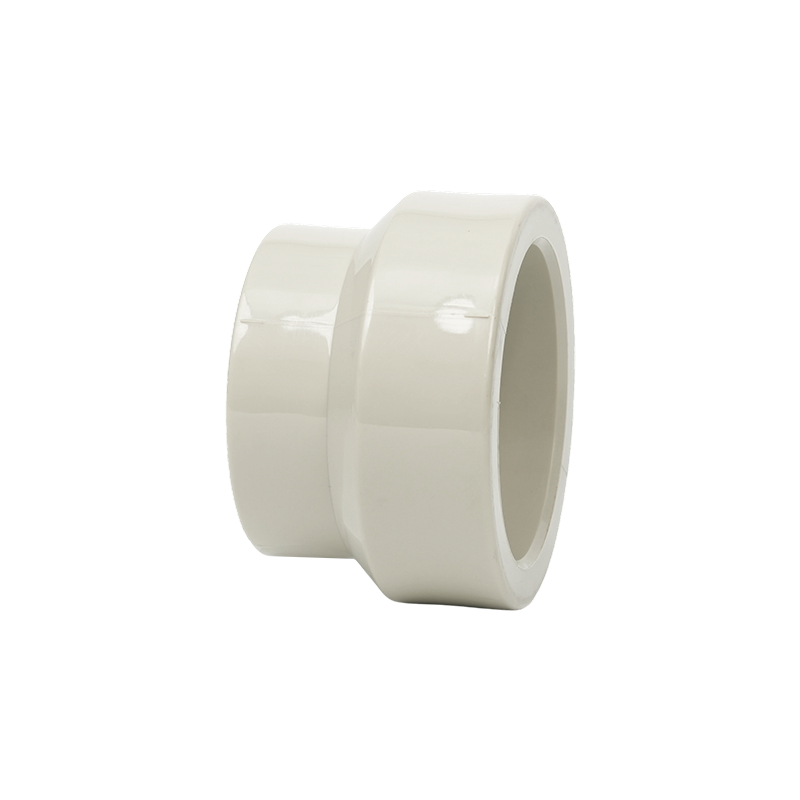
این اتصال برای کاهش اختلال جریان در طول انتقال قطر طراحی شده است. طراحی کا...
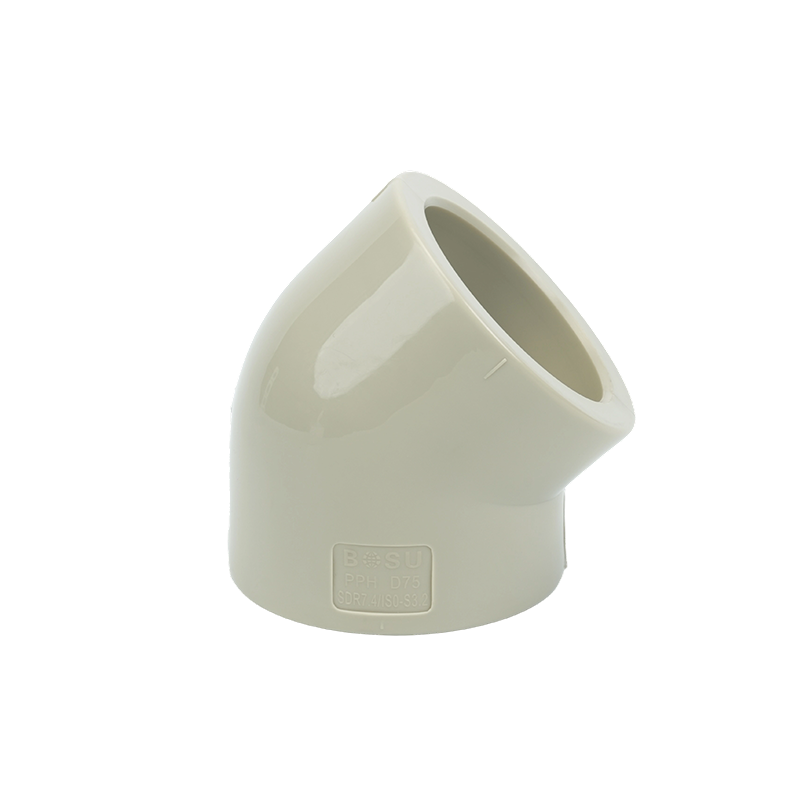
1. این اتصالات برای تغییر جهت خط لوله در زاویه 45 درجه استفاده می شود. سور...
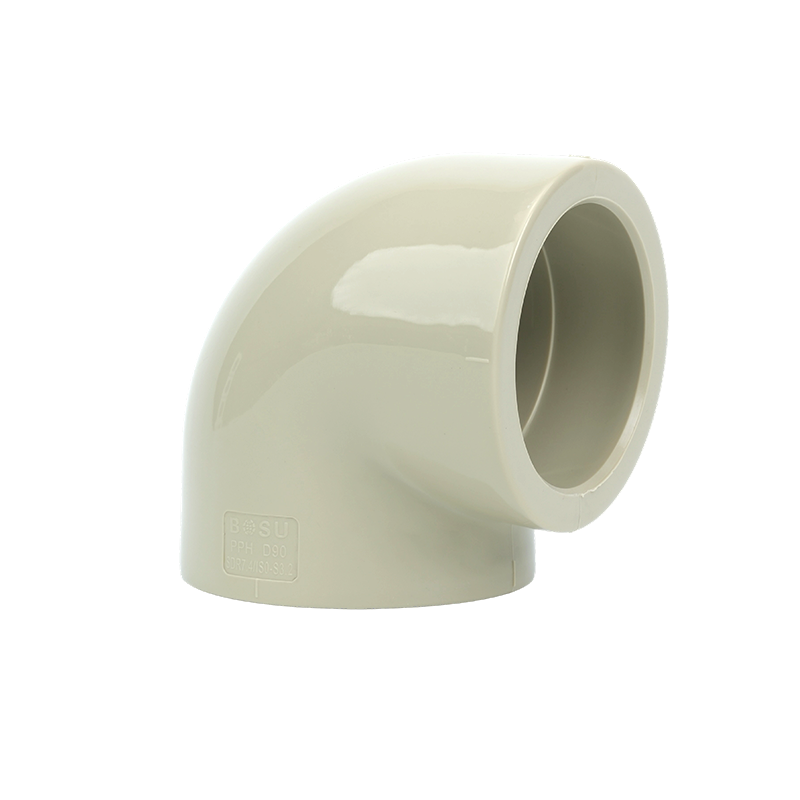
1. این اتصالات برای تغییرات جهت 90 درجه در خطوط لوله طراحی شده است و برای کار...
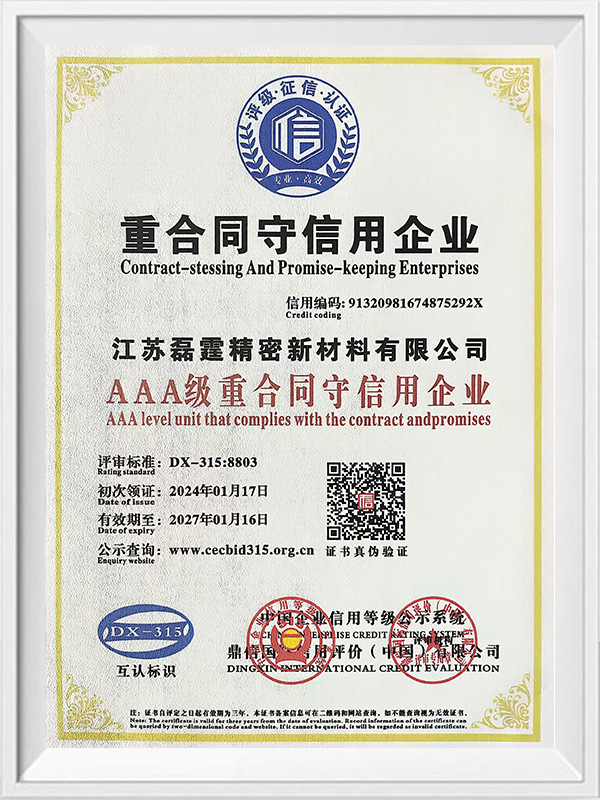
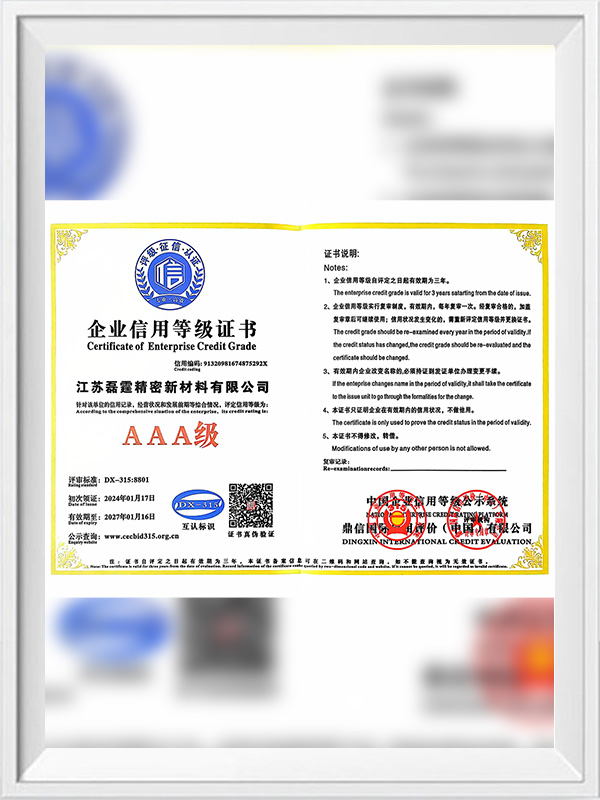
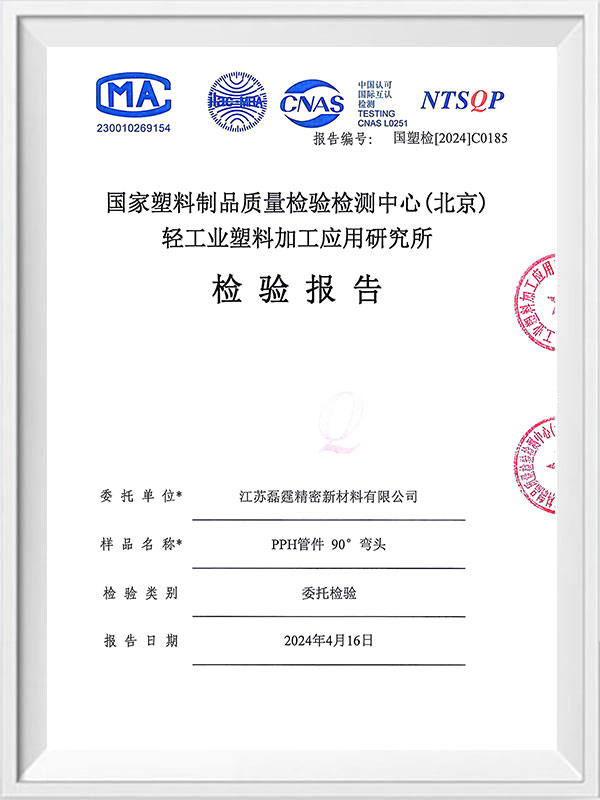
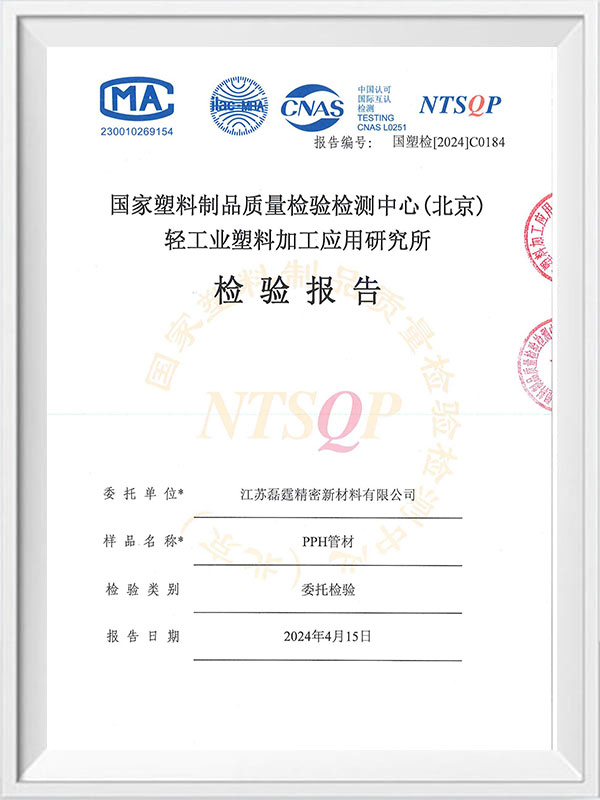
یک خدمه خاموش در یک کارخانه مواد شیمیایی قبل از راه اندازی مجدد یک کار باقی مانده بود: یک واشر نشتی را در یک شیر دوازده متری داخل یک خط PPH کاملاً جوش داده شده جایگزین کنید. برش لوله به معنای یک قرقره جدید، یک جوش جدید، یک انتظار خنک کننده و یک آزمایش فشار دوم، چهار ساعت اضافی بر اساس یک برنامه زمانی بود که هیچ چ...
نمایش بیشترخرید یک شیر توپی پلاستیکی با پرسیدن "آیا آنها را می فروشید؟" این است که چگونه پروژه ها دو بار پرداخت می کنند. چیزی که در واقع تصمیم میگیرد که آیا یک شیر توپی پلاستیکی به مدت پنج سال بیصدا کار میکند یا در سال اول از کار میافتد، مواد بدنه، الاستومر آببند و نحوه اتصال بدنه شیر به لوله است - نه قیمت واحد در برگه...
نمایش بیشتردو فیتر، یک سیم پیچ 2 عددی در لوله PVDF و یک جعبه آداپتور فلنجی DN 50. همه چیز طبق برنامه می رسد و هیچ چیز مناسب نیست: اندازه لوله 60.3 میلی متر در خارج است، در حالی که آداپتور برای قطر خارجی 50 میلی متر ماشین کاری شده است. هیچ کدام از این برچسب ها اشتباه نیست. قطعات به سادگی متعلق به دو سیستم اندازه گیری متفاوت ...
نمایش بیشتر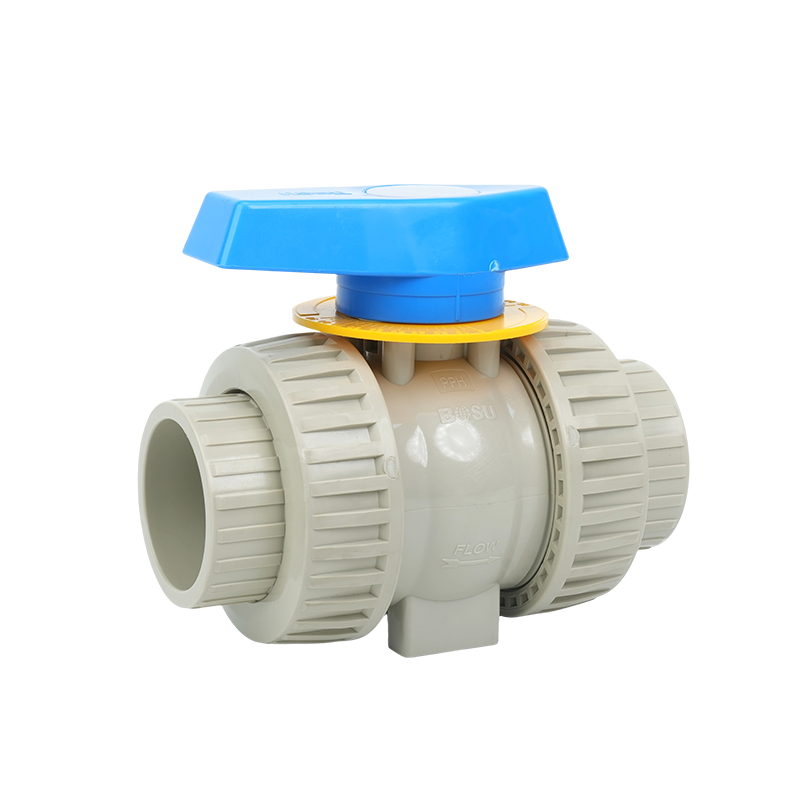
1. ویژگی های محصول: عملکرد نشانگر دسته شخصی، نصب LOGO، رسانه و غیره در پوشش ش...
نمایش بیشتر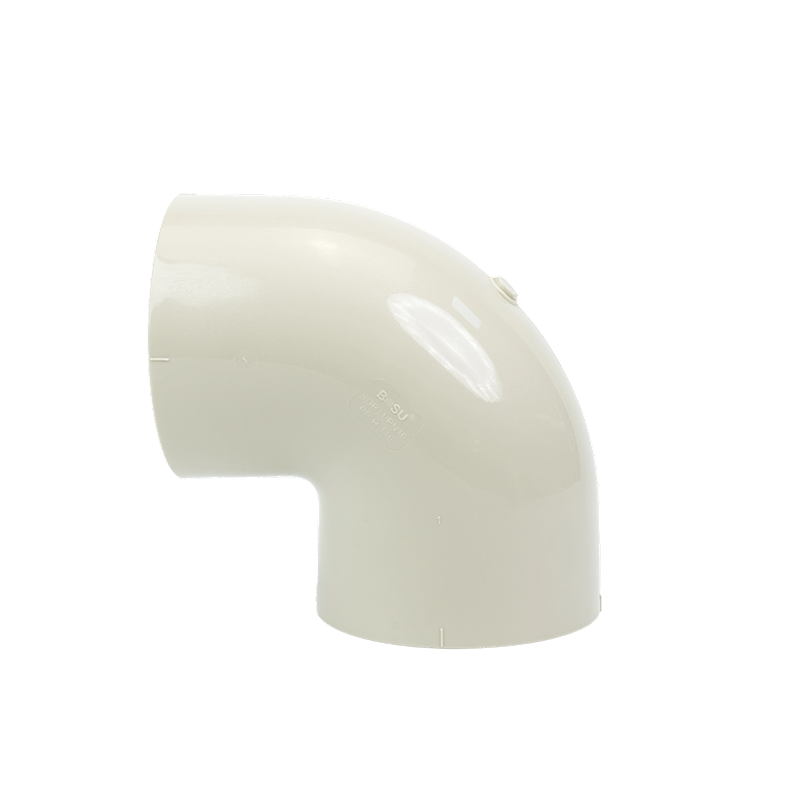
این زانویی جوشی پس از نصب ظاهری براق و با کیفیت را ارائه می دهد. مشخصات مح...
نمایش بیشتر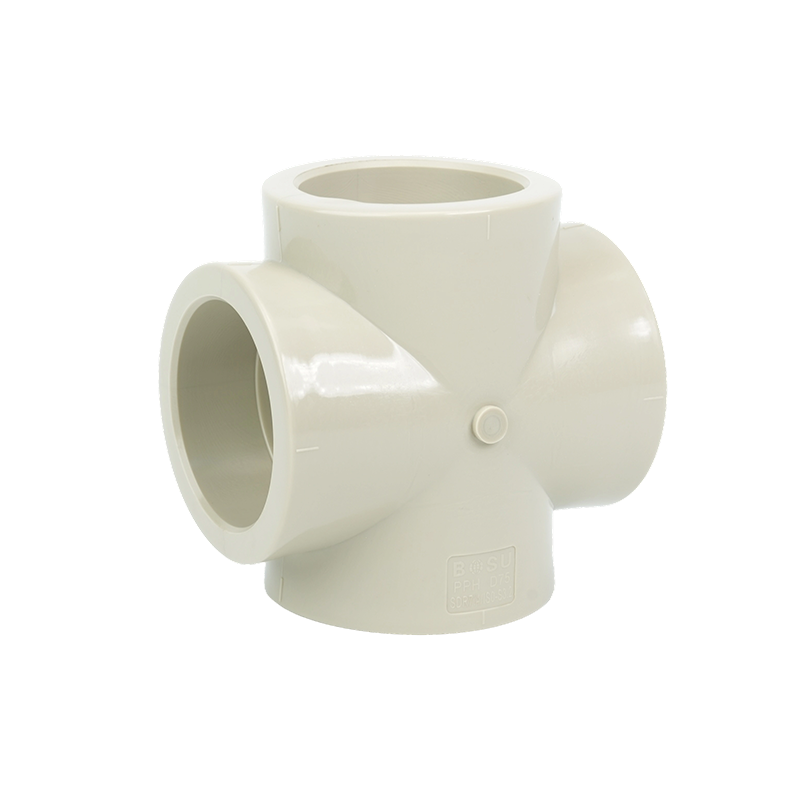
1. برای اتصال چهار لوله با قطر یکسان که عمود بر هم متقاطع می شوند استفاده می ...
نمایش بیشتر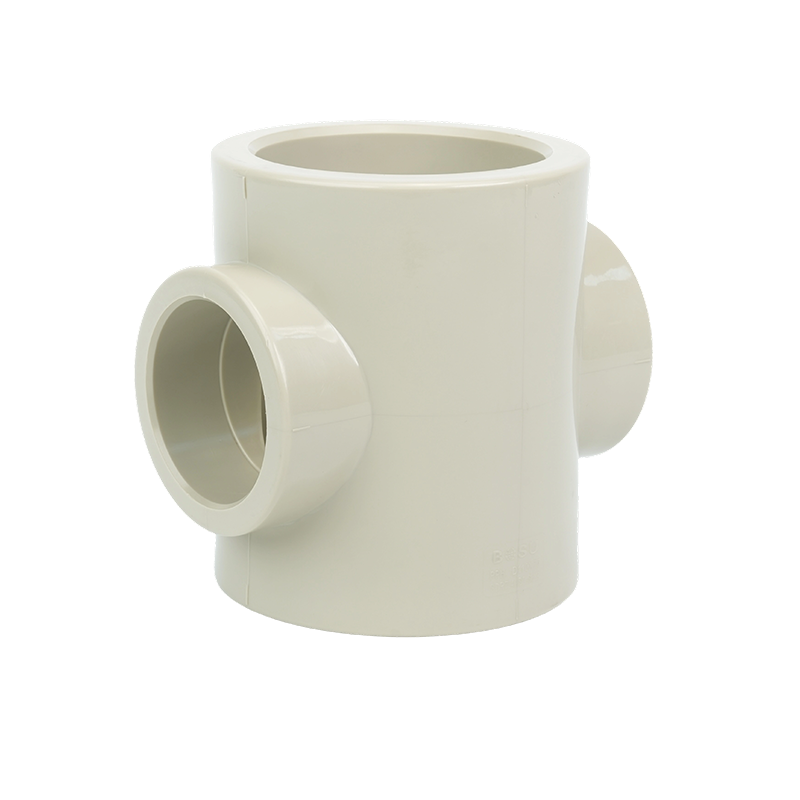
1. برای اتصال چهار لوله با قطرهای مختلف که به طور عمود بر هم متقاطع هستند ...
نمایش بیشتر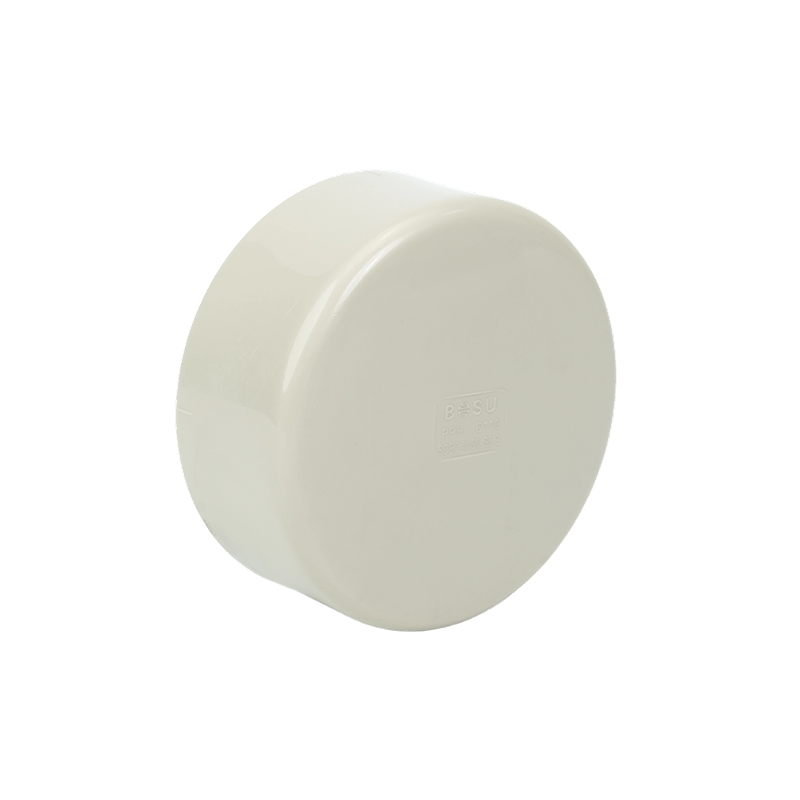
1. بادوام، مقاوم در برابر خوردگی، سبک وزن، مورد استفاده برای آب بندی خطوط لول...
نمایش بیشتر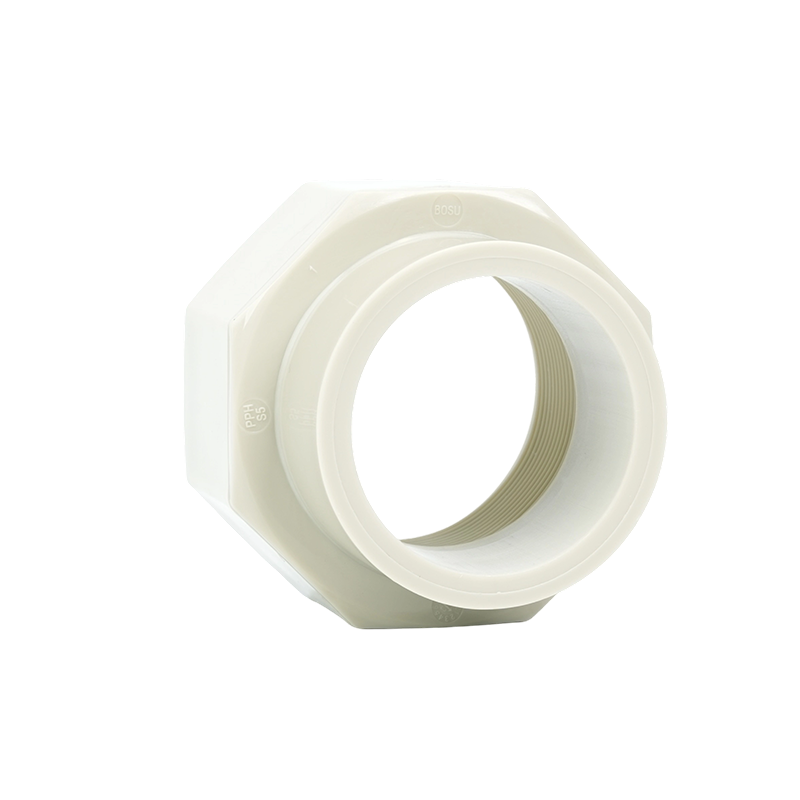
1. این محصول دارای نصب سریع، ایمن و کارآمد است. دیوارهای صاف داخلی و خارجی آن...
نمایش بیشترWhat are the key points of installation and welding processes for β-PPH Fittings?
1. Surface Cleaning and Cut Quality
Before installation, oil, dust, and rust must be thoroughly removed from the surfaces of pipes and fittings to ensure a clean contact surface.
Pipe ends must be cut squarely using a specialized cutting tool to ensure a perpendicular, burr-free end face for optimal interlocking strength.
2. Selection of Appropriate Connection Method
For β-PPH materials, two methods can be used: hot-melt welding (electrofusion) or adhesive bonding. Hot-melt welding is the most commonly used process, achieving a leak-free and reliable connection.
3. Key Welding Process Parameters
Heating Temperature: Generally controlled between 210℃ and 230℃ to ensure the material is fully softened without thermal degradation.
Pressure Holding Time: Maintain pressure for 8–12 seconds after heating to allow the melt to fully fill and form a uniform weld.
Cooling: Allow to cool naturally for at least 30 seconds after welding to avoid rapid cooling that could cause internal stress.
4. Quality Inspection and Leak Prevention Measures
After welding, conduct an airtightness test (such as helium leak detection or hydrostatic test) to confirm there are no leaks before putting the pipe into use.
Inspect the weld for bubbles, cracks, or incomplete fusion; re-weld if necessary.
How to select the specifications of β-PPH Fittings based on media type, working pressure, and temperature?
1. Media Corrosivity
For corrosive media such as strong acids and alkalis, thicker wall fittings or corrosion-resistant β-PPH modified materials should be used to resist chemical attack.
For neutral or weakly corrosive media (such as pure water and steam), standard wall thickness fittings can be used.
2. Matching Working Pressure and Temperature
The long-term working temperature range of β-PPH pipes is -20℃ to +100℃, and the short-term maximum withstand temperature is 110℃. Increased temperature significantly reduces pressure resistance; the maximum working pressure (MOP) at 60℃ is approximately 50% of the nominal pressure. When selecting a pipe fitting, the design pressure (usually 1.25 times the highest working pressure) should be considered, along with a temperature correction factor, to ensure that the fitting does not exceed the material's pressure resistance limit under actual operating conditions.
3. Wall Thickness and Nominal Size
Select the appropriate nominal diameter (DN) and wall thickness (PN) based on the viscosity, flow rate, and system pressure drop requirements of the medium.
For high-pressure and low-temperature environments, PN16 and above with thicker walls are recommended; under normal temperature and pressure, PN10–PN12 is sufficient.
4. Influence of Installation Method on Selection
Hot-melt welding has relatively relaxed requirements on pipe wall thickness, but welding quality must be ensured; flange connections have higher requirements on pipe wall thickness and require matching with appropriate flange thickness and bolt specifications.
محصولات
اطلاعات شرکت
آدرس: شماره 55 جاده هایچوان، منطقه فناوری پیشرفته، شهر دانگ تای، استان جیانگ سو، چین
موبایل: +86 137 7009 5258
تلفن: +86-515-85479999
ایمیل: [email protected]
ما مشتاق شنیدن نظر شما هستیم!